Reception.
BAR, HOLLOW AND FORGING STOCK BOOKED AGAINST AN APPROVED HEAT. MILL CERTIFICATES ARE READ BEFORE THE STRAPPING COMES OFF. HOLD · PMI ON RECEIPT
Preparing the opening shot 000%
Heavy-duty capabilities
Om Tubes & Fittings Industries manufactures tube fittings, valves and instrumentation tubing in Mumbai, India. Explore the range and prepare your enquiry with our specification guide.

High-vibration-resistant, gaugeable double-ferrule design giving leak-tight integrity across impulse and sample lines.
Review fitting specs→
Precision-machined from solid forged bar stock — no casting defects — for needle, ball and multi-valve manifold builds.
Source valve packages→
Anti-vibration coned-and-threaded connections for wellhead control panels and injection skids.
Inquire for skid pricing→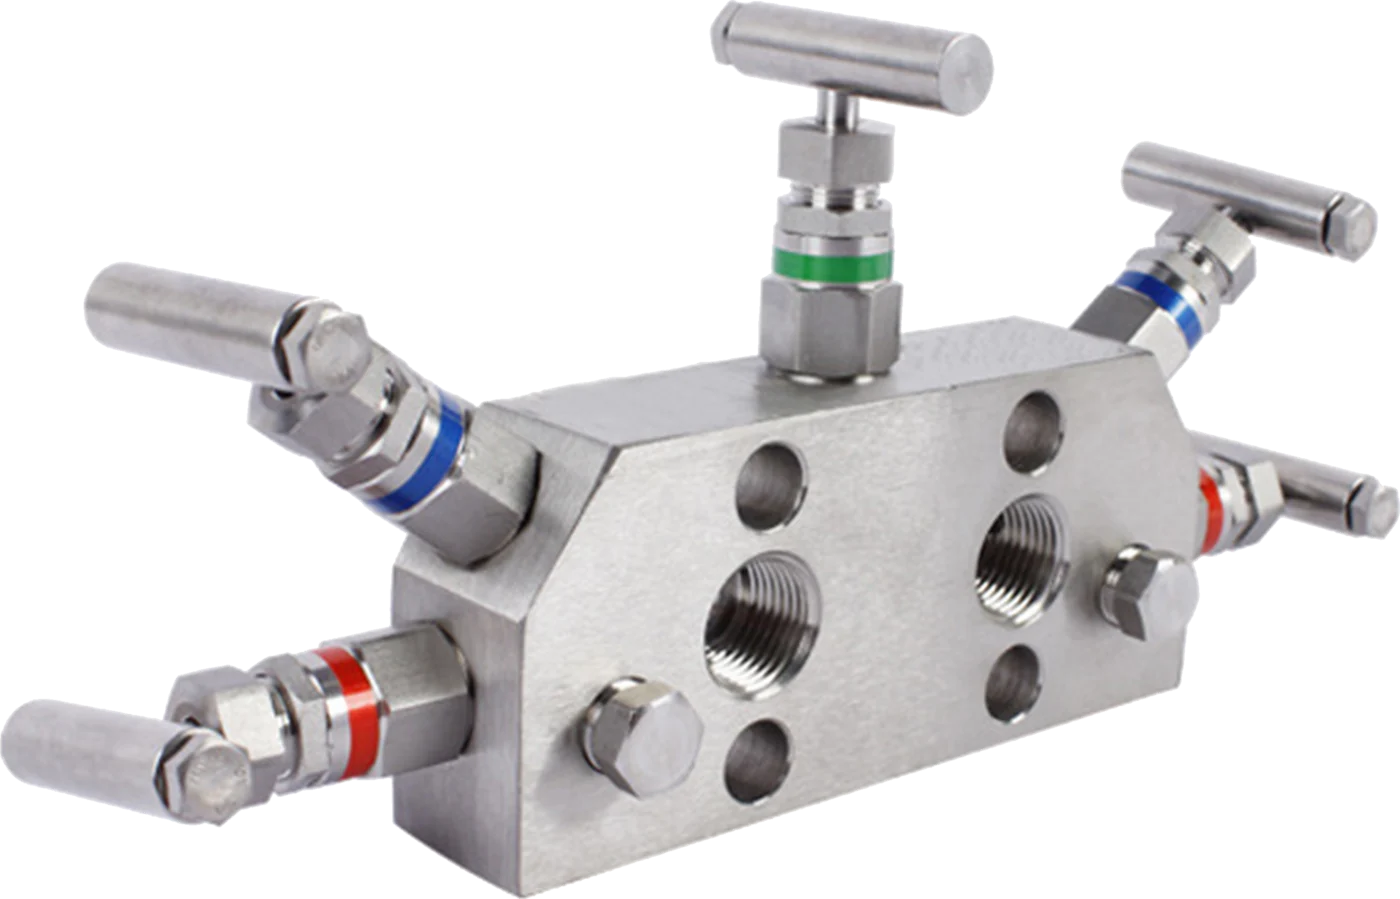
Compact single-body construction, eliminating multi-joint leak paths in hydrocarbon containment.
Request DBB datasheet→
Bright-annealed seamless straight lengths and long coils, prepped for field bending and orbital welding.
Browse alloy grades→How it works — bar to bundle
All seven stages, in detail→Qualifications
Certification is not a badge on a homepage. Every consignment leaves with the documents that let your inspector accept it without a phone call.
The OM6 fitting, part by part
A ¼-inch OM6 union elbow in 316L, straight off the line. Follow this fitting from the outside in, then onto the test bench.
What is inside the nut
Scroll to open one end of the elbow and reveal the two ferrules. Select a part to explore its role.
The elbow body turns the flow through 90 degrees and provides the seat for the front ferrule.
Before the bench, the standard
ASTM F1387-23 puts the connection through repeated assembly, pressure, bending and more. Explore what each test asks of the fitting.
Ask for the test reportFrom the part to the proof
The connection is assembled onto the tube. Now the pressure rises. Watch the actual bench footage and follow what happens to the joint.
Bench camera · Taloja test cell
The connection, after the test
The wall failed away from the joint. The ferrules held the tube, and the connection stayed sealed.


Examination · Dimensions, finish and marking are checked before the loading tests begin.
Scroll to follow the elbow · or choose a chapter below.
Field deployments
Five sectors take the bulk of what leaves the plant. Each one sets its own corrosion, temperature and pressure case — and its own certificate trail.
Christmas trees, wellhead manifolds, top-side skids and subsea tie-backs — NACE MR0175 compliant.
Hydrocracking units, delayed coking, catalytic reformers and high-temperature flare lines.
Ammonia, urea synthesis and aggressive acid process piping.
Boiler superheater tubes, high-pressure steam distribution and condenser lines.
Ballast water treatment, FPSO topside piping and high-salinity seawater intake.
Streamlined procurement
Eliminate single-source supply-chain bottlenecks. Drop your project MTO or competitor part numbers into our cross-reference engine — our engineers match exact technical equivalents (Swagelok®, Parker®, Parker Autoclave®) and return a fully compliant, itemised quote within 24 hours.